1
Section 5: Torch Consumables and Cutting Charts
Spirit II User’s Manual
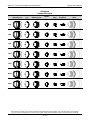
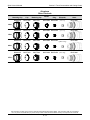
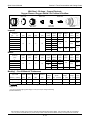
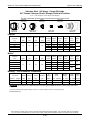
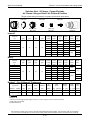
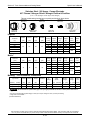
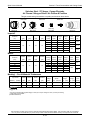
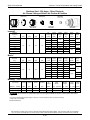
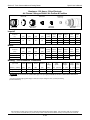
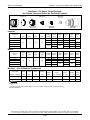
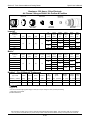
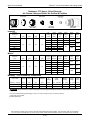
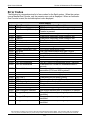
Stainless Steel - 70 Amps - Copper Electrode
H17 Plasma / Nitrogen Shield / Nitrogen Preflow & Postflow
(H17 = 17.5% Hydrogen / 32.5% Argon / 50% Nitrogen)
This gas combination gives the best cut quality and minimum dross levels
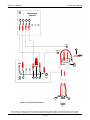
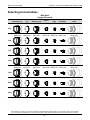
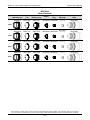
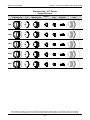
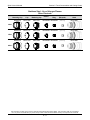
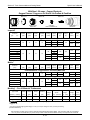
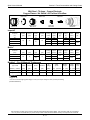
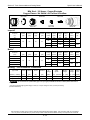
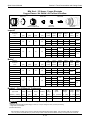
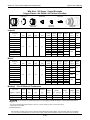
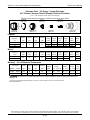
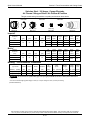
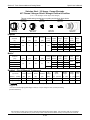
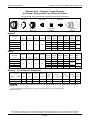
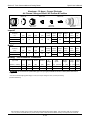
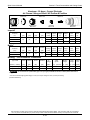
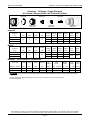
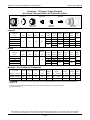
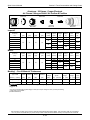
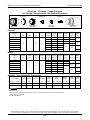
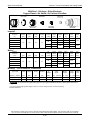
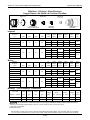
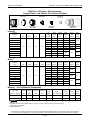
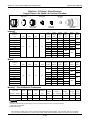
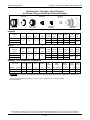
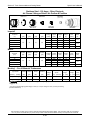
Shield Cap
BK277150
Outer Cap
BK284150
Nozzle
BK277124
Electrode
BK277132
Retaining Cap
BK277113
Swirl Ring
BK277140
Imperial*
Torch Head
BK279100
Material
Thickness
Preflow
Plasma
Shield
Postflow
Arc
Voltage
Travel
Speed
Cutting
Height
Pierce
Height
Pierce
Time
Kerf
Width
(in)
(psi)
(psi)
(psi)
(psi)
(volts)
(ipm)
(in)
(in)
(msec)
(in)
3/16
35
65
30
60
135
80
.100
.200
300
.090
Material
Thickness
Preflow
Plasma
Shield
Postflow
Arc
Voltage
Travel
Speed
Cutting
Height
Pierce
Height
Pierce
Time
Kerf
Width
(mm)
(psi)
(psi)
(psi)
(psi)
(volts)
(mm/m)
(mm)
(mm)
(msec)
(mm)
5
35
65
30
60
135
2030
2.5
5.1
300
2.3
Metric*
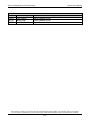
Marking* – For All Material Thicknesses
Type of Gas
Preflow
Plasma
Shield
Postflow
Arc
Voltage
Travel
Speed
Marking
Height
(ipm) (mm/min)
(in)
(mm)
Initial
Height
Pierce
Time
(Plasma)
(Shield)
(psi)
(psi)
(psi)
(psi)
(volts)
(in) (mm) (msec)
Nitrogen
Nitrogen
N/A
25
25
N/A
135
250
6350
.096
2.4
.100
2.5
0
Argon
Nitrogen
N/A
50
25
N/A
80
100
2540
.130
3.3
.100
2.5
0
WARNING Do not connect H17 (combustible gas) as an input gas (Pre/Postflow, Plasma, or Shield) at the same time as
Oxygen or Air.
* Use an arc transfer height (ignition height) of .150” (3.8 mm) for cutting and .100” (2.5 mm) for marking.
(Revised 04/26/2013)
This information is subject to the controls of the Export Administration Regulations [EAR]. This information shall not be provided to
non-U.S. persons or transferred by any means to any location outside the United States contrary to the requirements of the EAR.
5-24