1
Chapter 6 Cutter Compensation
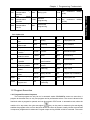
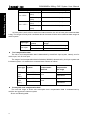
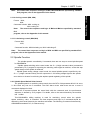
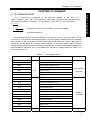
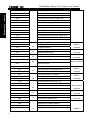
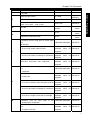
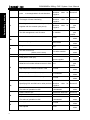
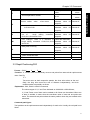
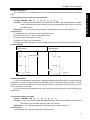
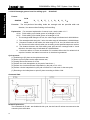
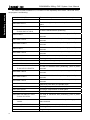
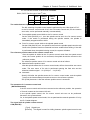
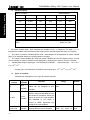
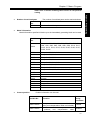
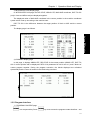
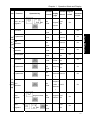
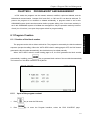
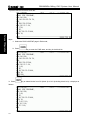
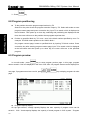
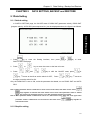
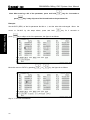
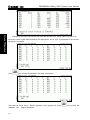
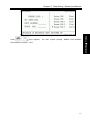
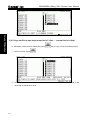
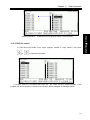
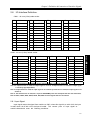
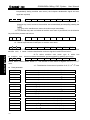
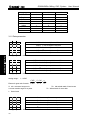
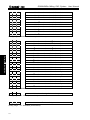
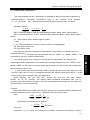
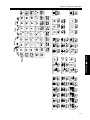
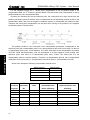
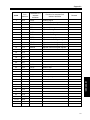
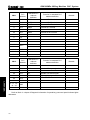
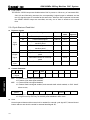
Geometric(H )
Wearing(H)
Geometric(D)
Wearing(D)
01
…
…
…
…
…
…
…
…
…
07
…
…
2.000
0.000
08
…
…
…
…
…
…
…
…
…
32
…
…
…
…
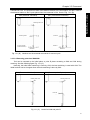
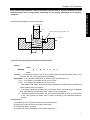
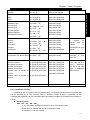
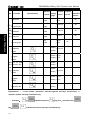
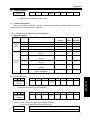
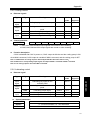
Programming
NO.
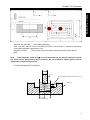
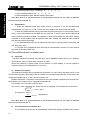
Programs:
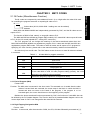
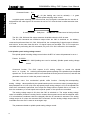
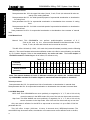
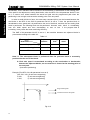
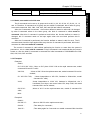
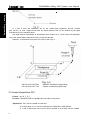
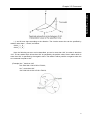
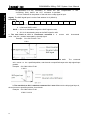
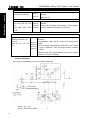
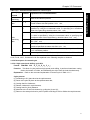
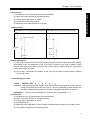
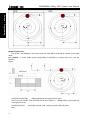
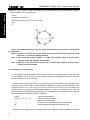
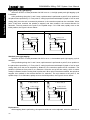
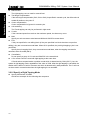
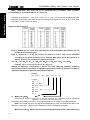
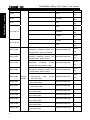
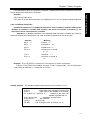
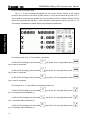
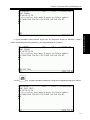
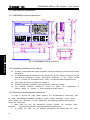
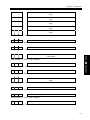
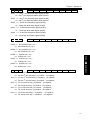
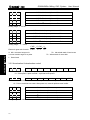
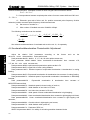
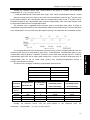
N0 G92 X0 Y0 Z0; Tool are positioned at start position X0, Y0 and Z0 when the absolute
coordinate system is specified
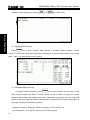
N1 G90 G17 G00 G41 D07 X250.0 Y550.0; Start-up cutter, the tool is shifted to the tool path by
the distance specified in D07, geometric radius of
D07 is set to 2.0mm, tool wearing 0, then the tool
radius is 2mm.
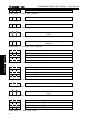
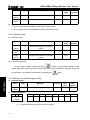
N2 G01 Y900.0 F150;
Specifies machining from P1 to P2
N3 X450.0;
N4 G03 X500.0 Y1150.0 R650.0;
N5 G02 X900.0 R-250.0;
N6 G03 X950.0 Y900.0 R650.0;
N7 G01 X1150.0;
N8 Y550.0;
N9 X700.0 Y650.0;
N10 X250.0 Y550.0;
N11 G00 G40 X0 Y0;
position (X0, Y0)
Volume I
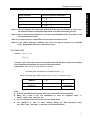
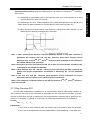
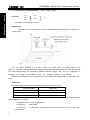
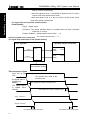
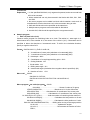
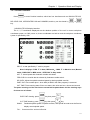
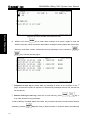
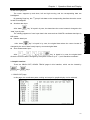
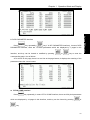
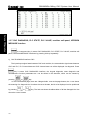
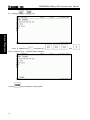
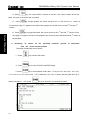
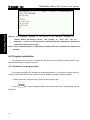
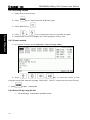
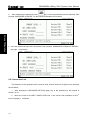
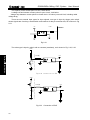
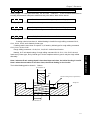
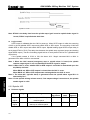
Perform tool setting in the mode of offset cancellation, after finishing the tool setting, and set the
tool radius D in OFFSET page.
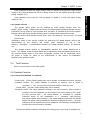
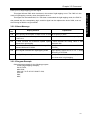
Table.4-2
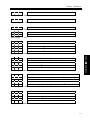
Specifies machining from P2 to P3
Specifies machining from P3 to P4
Specifies machining from P4 to P5
Specifies machining from P5 to P6
Specifies machining from P6 to P7
Specifies machining from P7 to P8
Specifies machining from P8 to P9
Specifies machining from P9 to P1
Cancels the offset mode, the tool is returned to the start
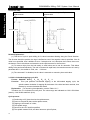
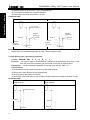
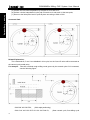
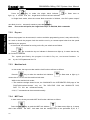
6.2 Offset Path Explanation for Cutter Radius Compensation
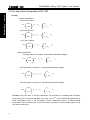
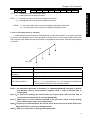
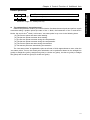
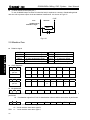
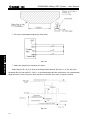
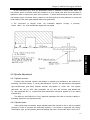
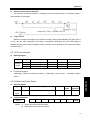
6.2.1 Conception for inner side or outer side
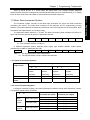
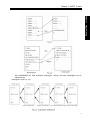
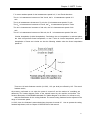
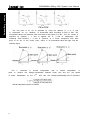
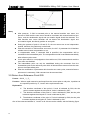
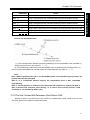
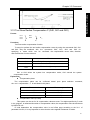
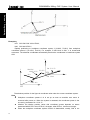
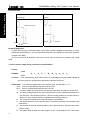
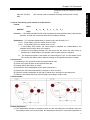
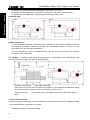
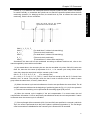
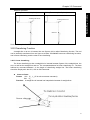
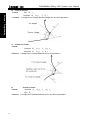
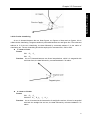
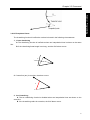
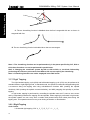
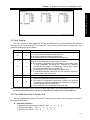
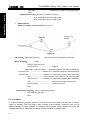
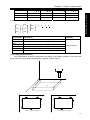
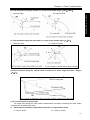
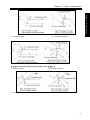
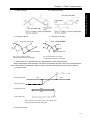
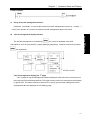
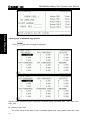
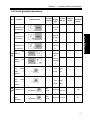
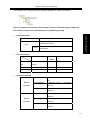
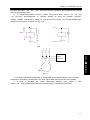
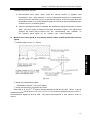
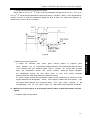
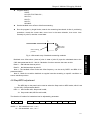
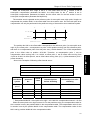
“Inner side” and “outer side” will be employed in the following explanations. When an angle
of intersection created by tool paths specified by move commands for two blocks is over or equal
to 180°, it is referred to as “inner side”. When the angle is between 0° and 180°, it is referred to
as “outer side”.
145