1
E.
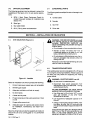
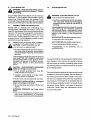
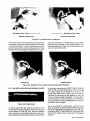
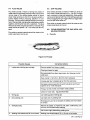
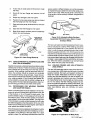
Excessive Penetration
(Burn-Through)
Figure
9-12. Excessive Penetration
Possible Causes
1.
Corrective Actions
Excessive heat input.
Select lower voltage range and reduce wire speed.
Increase travel speed.
F.
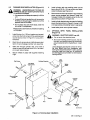
Cracks in Weld Metal
Possible Causes
1.
Corrective Actions
Improper joint preparation.
preparation and design must be ade
provide access to the bottom of the groove while
maintaining proper welding wire extension and arc characteris
Material too thick. Joint
quate
to
tics.
2.
Heat
input
shrinkage
too
high causing
Select lower voltage range and reduce wire speed.
excessive
and distortion.
Increase travel
G.
speed.
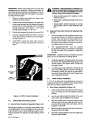
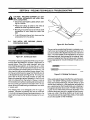
Waviness of Bead
Figure
9-13. Waviness of Bead
Corrective Actions
Possible Causes
1.
Welding
2.
Unsteady
H.
wire extends too far out of nozzle.
Welding wire should extend 1/4
Support
hand.
hand
on
in.
(6 mm)
.
out of nozzle.
solid surface.
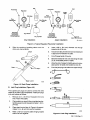
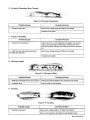
Humping
.
Figure
9-14.
Humping
Corrective Actions
Possible Causes
1.
Excessive heat
input.
Select lower
voltage range
or
increase travel
speed.
Weld in small segments and allow to cool between welds.
OM-113 336 Page 39