1
Manual machining
5.4 Manual machining using cycles (functions)
Input fields
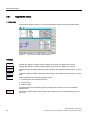
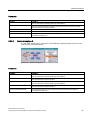
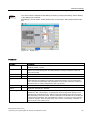
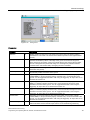
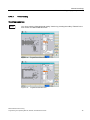
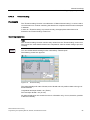
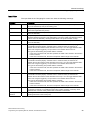
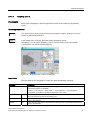
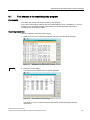
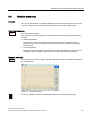
The input fields in the "Roughing F" screen form have the following meanings:
Parameter
Description
Length
l
Enter here the length of the end face to be cut, taking the contour start position
("Reference z0") in the longitudinal axis (Z axis) as the starting point.
Diameter
d1
External diameter of the end face to be cut (absolute position of the X axis in the
diameter).
Diameter
d2
Internal diameter of the end face to be cut (absolute position of the X axis in the
diameter).
Max. infeed depth
m1
Enter the maximum infeed depth for roughing. The internal infeed calculation
ensures that the infeed is as uniform as possible throughout the roughing operation.
This entry value represents the maximum value possible and is therefore not
exceeded.
Finishing allowance
m2
Finishing allowance in the X axis (m2x)
Finishing allowance in the Z axis (m2z)
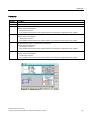
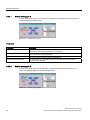
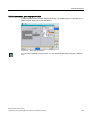
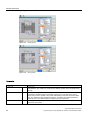
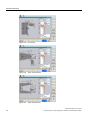
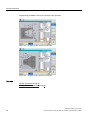
The following option is available for the position of the geometry:
Figure 5-61
100
Roughing cycle F, position "Outside left"
Manual Machine Plus Turning
Programming and Operating Manual, 06/2009, 6FC5398-6CP10-1BA0