1
Measuring Cycles for Milling and Machining Centers
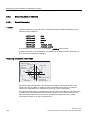
5.10 CYCLE996 workpiece: Measure kinematics
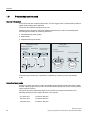
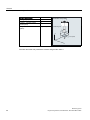
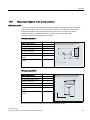
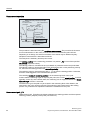
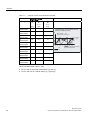
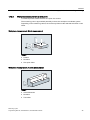
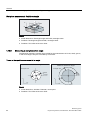
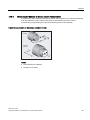
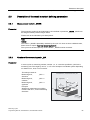
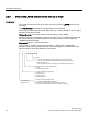
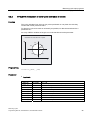
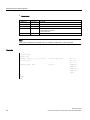
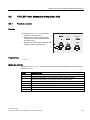
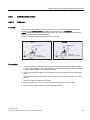
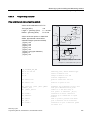
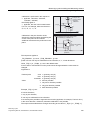
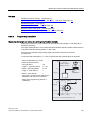
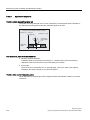
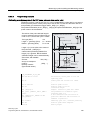
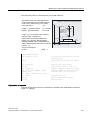
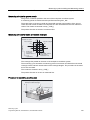
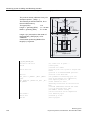
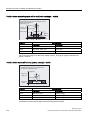
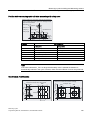
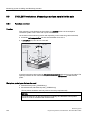
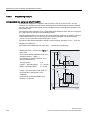
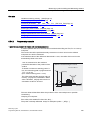
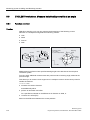
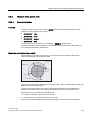
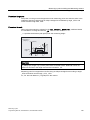
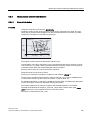
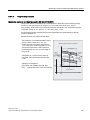
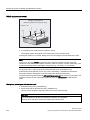
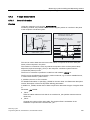
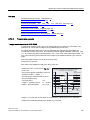
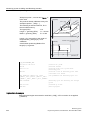
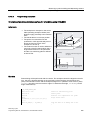
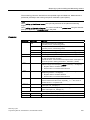
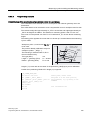
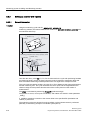
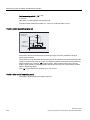
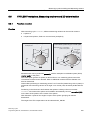
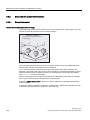
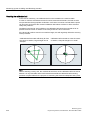
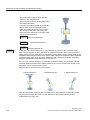
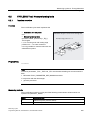
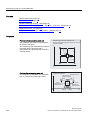
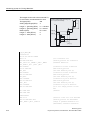
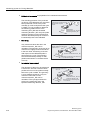
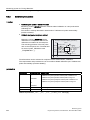
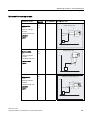
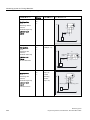
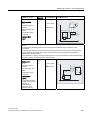
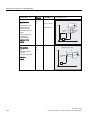
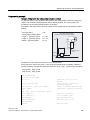
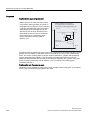
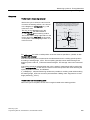
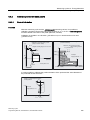
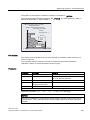
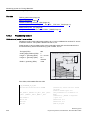
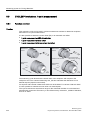
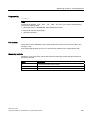
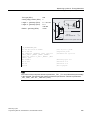
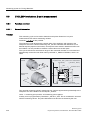
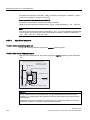
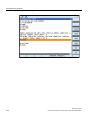
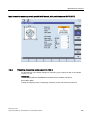
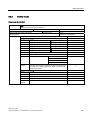
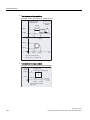
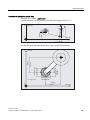
Start position
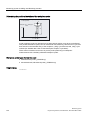
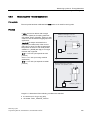
The starting position of the probe must be
approached by the user or from the user
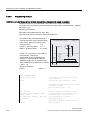
program (see example program).
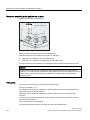
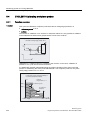
The probe must be prepositioned in the
direction of the tool orientation (ORI)
above the highest point of the calibration
ball (probe aligned with ball center point).
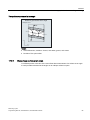
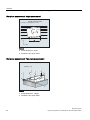
After approaching the starting position,
the distance (D) from the calibration ball
should be as short as possible.
25,
$
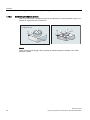
Note
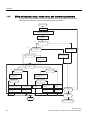
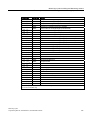
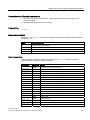
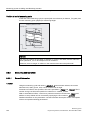
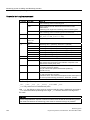
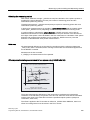
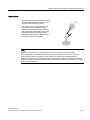
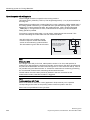
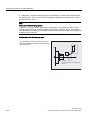
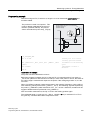
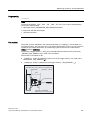
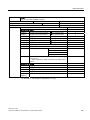
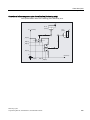
Measure kinematics is also possible with active 5-axis transformation (TRAORI).
As a prerequisite for Measure kinematics with active TRAORI, the vectors of the 5-axis
transformation must be roughly set. The positions for measuring the kinematics are
approached in the user program with active transformation. During the actual measurement
with the calibration ball, CYCLE996 switches off the transformation and switches it on again
after the measurement.
Measuring cycles
Programming Manual, 03/2009 Edition, 6FC5398-4BP10-2BA0
247