1
Specifications, Customization and Troubleshooting
9.4.3
9.4.4
•
PC Windows Control with integrated safety & manual overrides (PC not included,
Windows XP or Windows Vista is required). Computer control is integrated with an
operator control panel for spindle lockout, manual spindle controls, manual coolant control
and PC power control.
•
Digitizing & tool touch off (accessory) port, optically isolated.
•
Coolant or accessory AC outlet. The AC outlet for coolant is automatically controlled via
M-codes while the operator console offers a convenient manual override.
•
PC/Controller or accessory AC outlets, manually controlled on the operator console.
•
Power requirements – Machine tool: 115-130 VAC, 20amp single phase.
System
•
Complete RS-274 (G- & M-codes) implementation with virtually unlimited program size.
Conventional G- & M-code operations are complemented with manual mode operations,
operation wizards. Operation Wizards allow pocketing, surfacing, cutouts, drill patterns and
other standard operations to be completed without the need for addition software or manual
code writing.
•
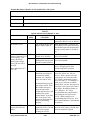
Supported codes include: G00 [Default]Positioning (Rapid Traverse), G01 Linear
Interpolation, G02 Circular/Helical Interpolation CW, G03 Circular/Helical Interpolation
CCW, G04 Dwell , G17 [Default] Circular Move XY Plane, G18 Circular Move ZX Plane,
G19 Circular Move YZ Plane, G20 [Default] 06 Inch Input, G21 Millimeter Input, G40
[Default] Cancel Cutter Compensation, G41 Cutter Compensation Left, G42 Cutter
Compensation Right, G50, G51 Scaling, G52 Special offset, G53 Work Offset Cancel,
G54-G59 Work Offset, G74 Incremental Input I, J, K, G75 [Default] Absolute Input I, J, K,
G80 [Default] Canned Cycle Cancel, G81 Spotting Drill Cycle, G82 Speed Peck Drill
Cycle, G83 Full Retract Peck Drill Cycle, G85 Boring Cycle, G86 Boring Cycle – Spindle
Stop, G87-89 User Definable, G90 [Default] Absolute Input, G91 Incremental Input, G92
Set Program Part Zero, M00 Program Stop, M01 Optional Program Stop, M02 Program
End, M03 Spindle Clockwise , M04 Spindle Counter-clockwise, M05 Spindle stop, M06
Tool change, M07/M08 Coolant, M09 All Coolant Off.
Options
The PCNC 770 comes preconfigured for low cost 4th axis addition. Software support, wiring,
cabinet holes and drive mount holes are all in place for an easy 4th axis addition.
A wide range of accessories such as tapping heads, probes, tool setting sensors are available.
9.5
Maintenance
9.5.1
Foreword – Understanding Machine Design
The PCNC 770 has been designed for user maintenance, but an important prerequisite to
effective maintenance is an understanding of some general machine design concepts. For many
owners the PCNC 770 is their first experience with a serious machine tool and they may be
unfamiliar with the ideas presented here. This section should be read and understood before
attempting any adjustments to the machine.
9.5.1.1
Machine Stiffness
Iron is a wonderful thing. In the context of the human experience, the iron and steel of your mill
seems exceptionally stiff and essentially immovable. Never the less, any physicist or material
scientist will tell you that iron is a Hookean material, meaning that it always obeys Hooks Law
32426 Rev C1-1
9-3
Using Tormach PCNC 770