1
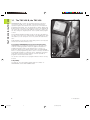
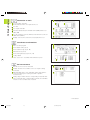
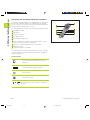
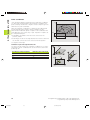
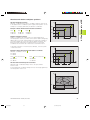
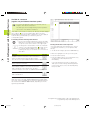
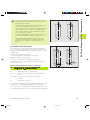
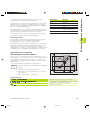
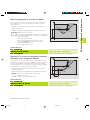
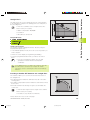
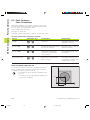
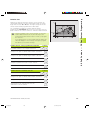
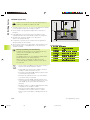
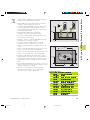
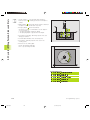
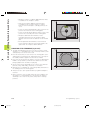
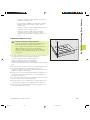
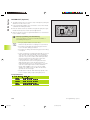
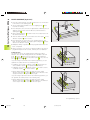
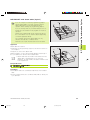
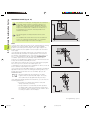
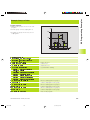
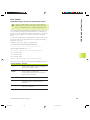
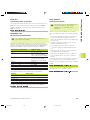
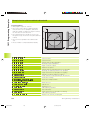
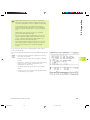
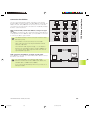
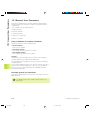
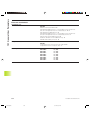
Program sequence
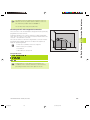
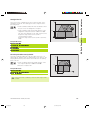
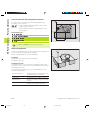
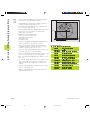
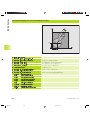
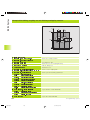
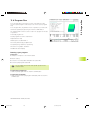
■ Pre-position the tool to the workpiece surface
Y
■ Enter the infeed depth in incremental values
■ Mill the contour
100
■ Repeat downfeed and contour-milling
R1
5
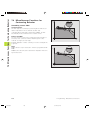
9.6 Programming Examples
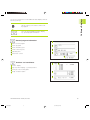
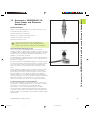
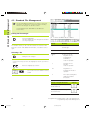
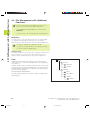
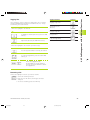
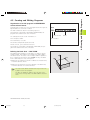
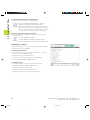
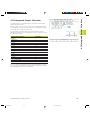
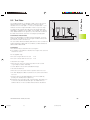
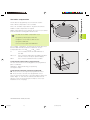
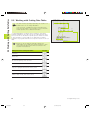
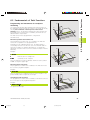
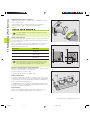
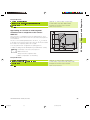
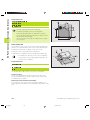
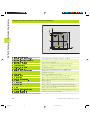
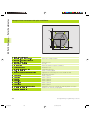
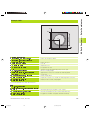
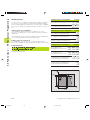
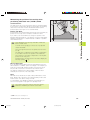
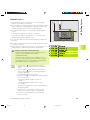
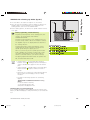
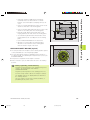
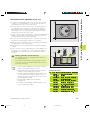
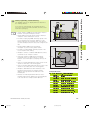
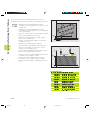
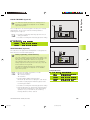
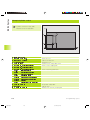
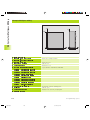
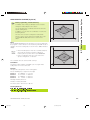
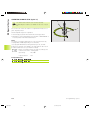
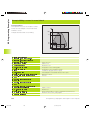
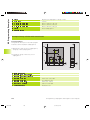
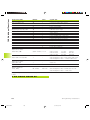
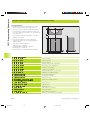
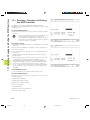
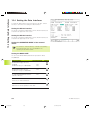
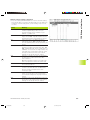
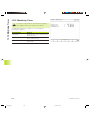
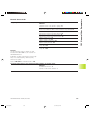
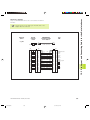
Example: Milling a contour in several infeeds
75
R18
30
R15
20
20
0
1
2
3
4
5
6
7
8
9
10
11
12
13
14
15
16
17
18
19
20
21
22
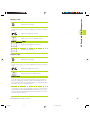
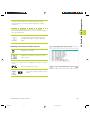
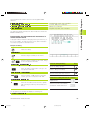
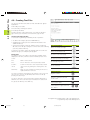
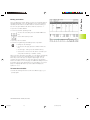
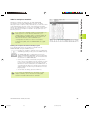
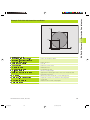
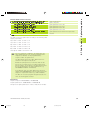
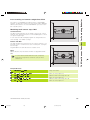
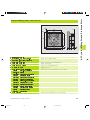
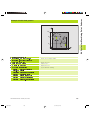
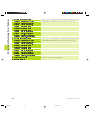
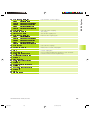
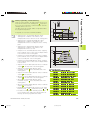
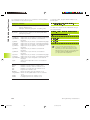
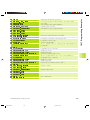
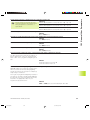
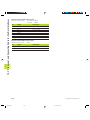
BEGIN PGM PGMWDH MM
BLK FORM 0.1 Z X+0 Y+0 Z-40
BLK FORM 0.2 X+100 Y+100 Z+0
TOOL DEF 1 L+0 R+10
TOOL CALL 1 Z S500
L Z+250 R0 F MAX
L X-20 Y+30 R0 F MAX
L Z+0 R0 F MAX M3
LBL 1
L IZ-4 R0 F MAX
APPR CT X+2 Y+30 CCA90 R+5 RL F250
FC DR- R18 CLSD+ CCX+20 CCY+30
FLT
FCT DR- R15 CCX+50 CCY+75
FLT
FCT DR- R15 CCX+75 CCY+20
FLT
FCT DR- R18 CLSD- CCX+20 CCY+30
DEP CT CCA90 R+5 F1000
L X-20 Y+0 R0 F MAX
CALL LBL 1 REP 4/4
L Z+250 R0 F MAX M2
END PGM PGMWDH MM
246
LKAP9.PM6
50
75
100
X
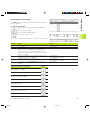
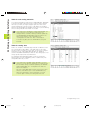
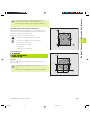
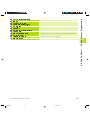
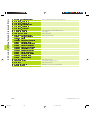
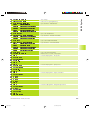
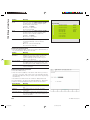
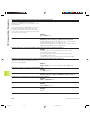
Define the tool
Call the tool
Retract the tool
Pre-position in the working plane
Pre-position to the workpiece surface
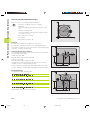
Set label for program section repeat
Infeed depth in incremental values (in the open)
Approach contour
Contour
Depart contour
Retract tool
Return jump to LBL 1; section is repeated a total of 4 times
Retract in the tool axis, end program
9 Programming: Subprograms and Program Section Repeats
246
30.06.2006, 07:04