1
User Manual
First, we should understand that the lower the layer height the more difficult it is to extrude filament. The
smaller the nozzle orifice the more difficult it is to extrude filament. These 2 factors determine the maximum
speed that we can print before the filament will strip at the extruder or jam in the hotend. Therefore increasing
one or both of them is the way to faster print speeds. However, there is a limit to both factors. We only supply
nozzles with an orifice diameter up to 1mm. The limitation will be that all corners will have a radius of .5mm and
won’t look very ‘square’. We can’t go bigger because the filament is only 1.65mm in diameter minimum and so
wouldn’t melt reliably if the orifice were larger. The maximum layer height is determined to be equal to the
nozzle orifice. See the chart below for the min/max layer heights of each nozzle by orifice size:
Layer
Nozzle
Min
Max
0.10
0.025
0.100
0.20
0.025
0.200
0.35
0.025
0.350
0.50
0.025
0.500
0.70
0.100
0.700
1.00
0.300
1.000
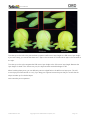
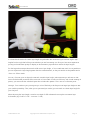
The lower the layer height the ‘higher’ the resolution of the print. This means that the higher the resolution, the
more difficult it is to visually see the layers of the print. The smaller the layers, the closer the printed parts will
resemble an injection molded piece. However, the time required to complete higher resolution prints scales
linearly with layer height (i.e. half the layer height will take twice as long).
orddistribution.com
Copyright 2015 ORD Solutions (Dist.) Inc.
Page 69