1
GSK983M Milling CNC System User Manual (Volume I: Specifications and Programming)
3.6 Compensation
3.6.1 Tool length compensation (G43, G44, G49)
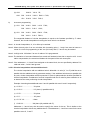
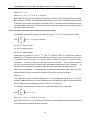
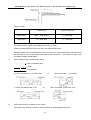
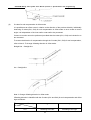
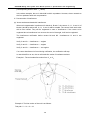
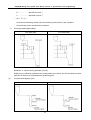
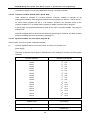
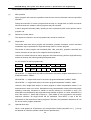
Using G43
Z—H—; or
G44
G43
H—;
G44
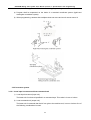
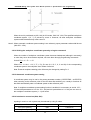
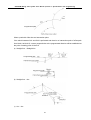
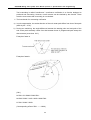
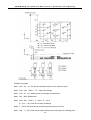
The end position of the axis Z move command is moved forward or backward by setting the
offset set in the offset stored. Using this function may set the difference between the tool length
estimated in programming and the actual one in service into the offset stored to achieve
compensation without changing the program. H instructs the offset set into the offset stored by
instructing the offsetting direction with G43 and G44.
4)
Offsetting direction
G43
Offset in + direction
G44
Offset in - direction
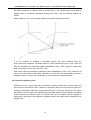
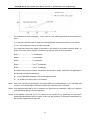
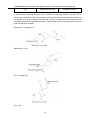
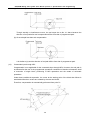
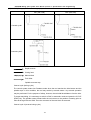
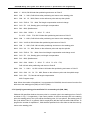
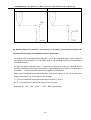
Whether in the situation of absolute or incremental command , the offset specified by H codes
and saved in the offset stored is added to the coordinates of the end point of the spindle move
command for G43 and detracted from it for G44. The calculated coordinates become the end
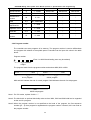
point of the coordinates. It may be illustrated in the same way when axis Z move command is
ignored as follows:
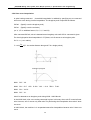
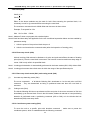
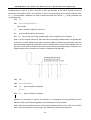
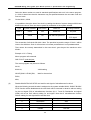
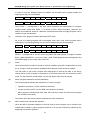
G43
G91
ZOH——;
G44
The offset is positive for G43 and negative for G44.
G43 and G44 are modal G codes and, when instructed, are always valid if no G codes in the same
group are coded. G 43 or G44 code is valid upon power on depends on parameter setting.
5)
Offset specifying
Offset number is specified with H codes. The offset set in the offset stored of the number is
added to or detracted from the programming value of axis Z. Offset number may be specified
with H00 or H200. The number of the D codes using tool radius compensation hits 32 (It is also
possible to choose 64, 90 or 200).
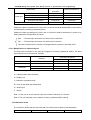
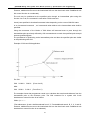
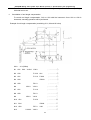
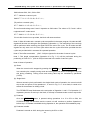
Offset corresponds to offset number and may be preset in the offset stored through MDI/LCD or
communicating operations. The setting range of the offset is as follows:
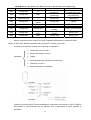
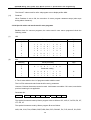
Offset
Input in mm
Input in inch
0mm~±999.999mm
0 inch~±999.999inch
62