1
Chapter 14
Axis Motion
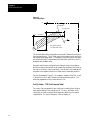
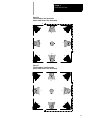
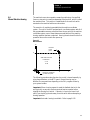
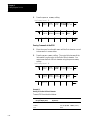
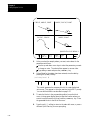
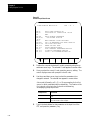
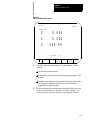
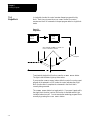
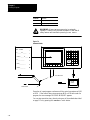
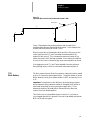
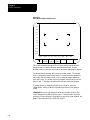
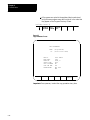
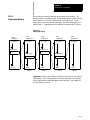
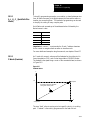
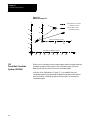
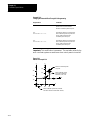
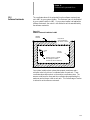
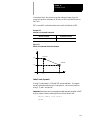
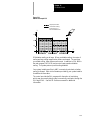
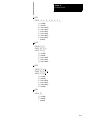
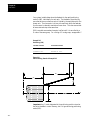
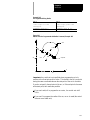
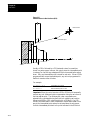
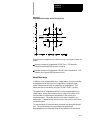
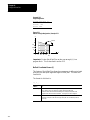
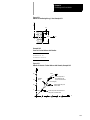
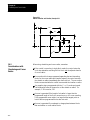
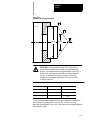
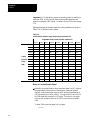
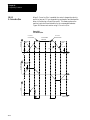
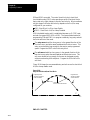
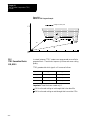
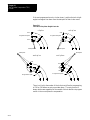
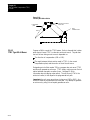
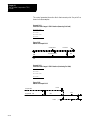
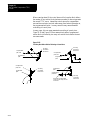
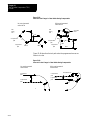
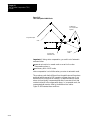
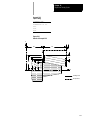
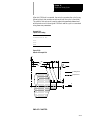
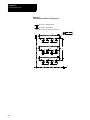
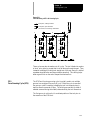
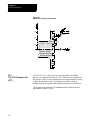
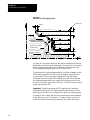
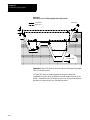
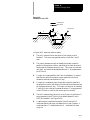
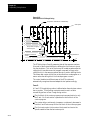
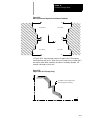
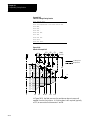
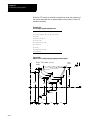
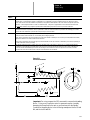
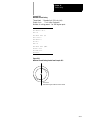
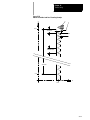
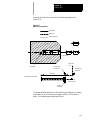
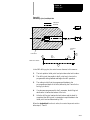
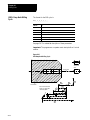
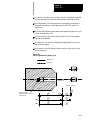
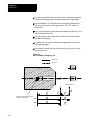
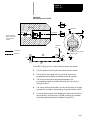
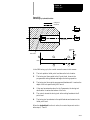
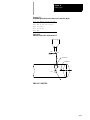
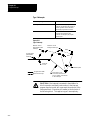
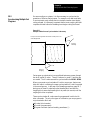
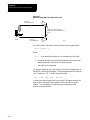
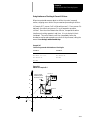
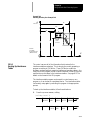
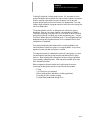
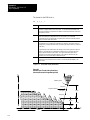
Figure 14.8
Automatic Return From Machine Home, Results of Example 14.7
X
Machine home
200
N30
150
N40
N30
N10
N20
100
50
Z
50
100
150
200
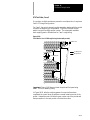
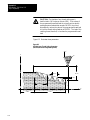
Important: When a G29 is executed, tool offsets and/or cutter
compensation are deactivated on the way to the intermediate point, and
they are re-activated when the axis moves from the intermediate point back
to the point indicated in the G29 block.
14.2.4
Machine Home Return
Check (G27)
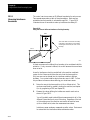
A G27 causes the control to move the axes at rapid directly to the machine
home position. Only the axes included in the G27 block are moved.
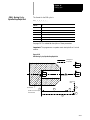
G27 X__ Z__;
The value entered with the axis name in the G27 block must be the
machine home coordinate for that axis. If it is not, no axis motion takes
place and the control issues the error message:
“INVALID ENDPOINT IN G27 BLOCK”
Aside from this endpoint check, the only difference between a G27 block
and a G00 block requesting a move to the machine home coordinates is
that the G27 is not modal. If G01, G02, or G03 modes were active before
the G27 was executed, they are reactivated immediately after the G27
block is completed.
G27 block commands are usually given after tool offset modes have been
cancelled.
14-16