1
Chapter 25
Thread Cutting
Programming Multipass Thread Cutting
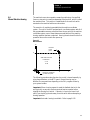
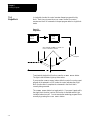
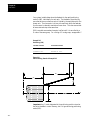
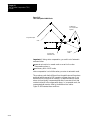
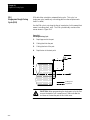
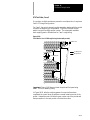
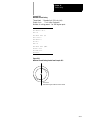
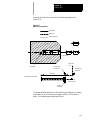
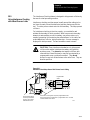
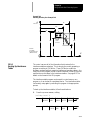
Before programming the G78 threading routine, the cutting tool must be
positioned to the point from which the routine is to be executed. This point
is the end-point of each complete cycle of the threading routine’s
execution.
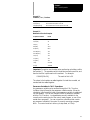
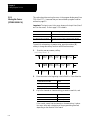
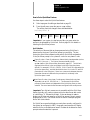
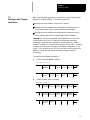
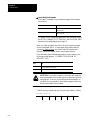
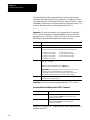
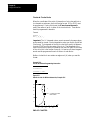
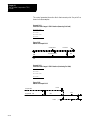
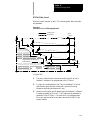
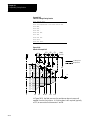
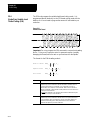
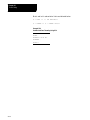
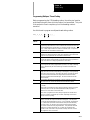
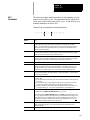
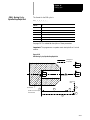
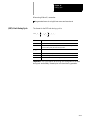
Use this format to program a multipass thread cutting routine:
G78X__Z__K__D__
F__
E
A__P__I__;
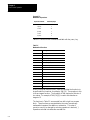
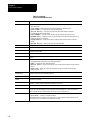
Where :
Is :
X:
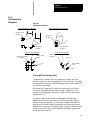
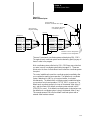
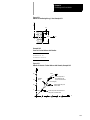
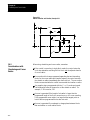
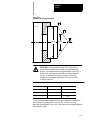
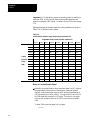
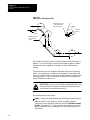
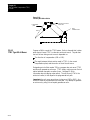
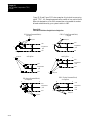
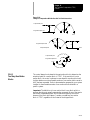
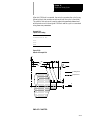
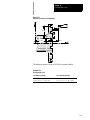
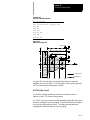
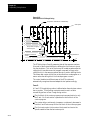
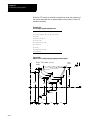
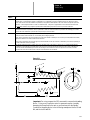
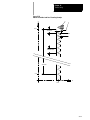
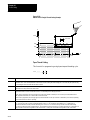
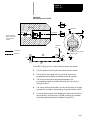
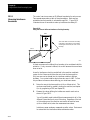
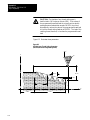
This parameter is the coordinate value of the root (depth) of the thread. If
programming a tapered thread, it is the coordinate value to be attained at the end
of the last threading pass (assume there is no chamfer cut at the end of the
pass). X values may be entered as a radius or a diameter value. X may also be
programmed as an incremental or absolute value.
Z:
This parameter is the Z coordinate value of the end of the thread cutting pass. Z
parameters are always entered as a radius value regardless of the current mode.
Z may also be programmed as an incremental or absolute value.
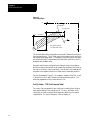
K:
This parameter is an unsigned value (always programmed as positive). It
programs the distance from the thread root (as determined by the X parameter to
the top of the thread. K is always programmed as a radius value.
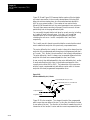
D:
This parameter programs the depth of cut (designated in radius) for the first pass.
It is an unsigned value (always programmed as positive). The depth of following
passes is determined by this value and the type of infeed selected with the P
parameter.
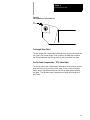
A:
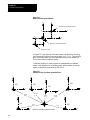
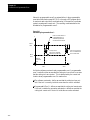
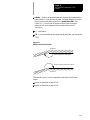
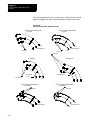
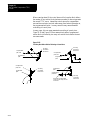
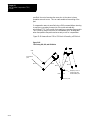
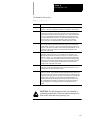
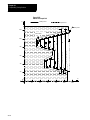
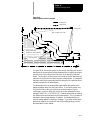
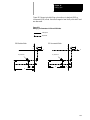
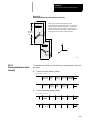
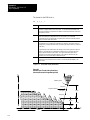
This parameter programs the angle of the tool tip. It must be entered as an
integer value from 0 to 120 (corresponding to 0-120 degrees). Not programming
a value for A is the same as A0. A0 would be the same as a plunge type infeed.
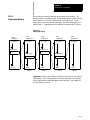
The value entered here determines the angle that the infeed moves makes,
which also determines the final thread angle. See the tool infeed section that
follows for details.
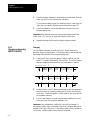
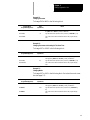
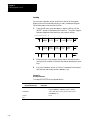
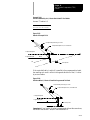
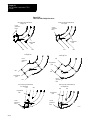
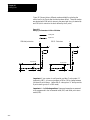
P:
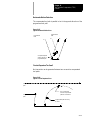
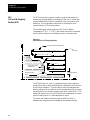
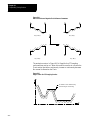
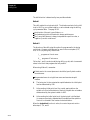
This parameter determines the tool infeed. It must be entered as an integer
value from one to four. See the tool infeed section that follows for details.
E,F:
This parameter may be entered by using either E or F for the thread lead
(as in G33).
If the E-word is programmed, its value (always unsigned) is equal to the number
of threads per inch or inches per thread (determined in AMP) regardless of
whether inch or metric mode is active at the time.
If the F-word is programmed, its value (always unsigned) is the thread lead in
inches per revolution or millimeters per revolution, depending on the mode in
which the control is operating.
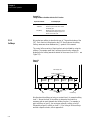
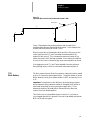
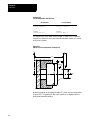
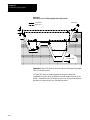
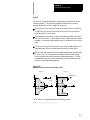
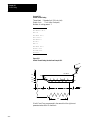
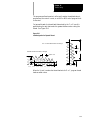
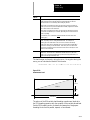
I
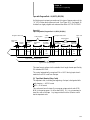
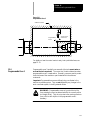
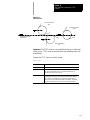
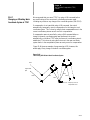
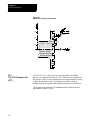
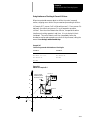
This is the change in radius of the thread (on the X axis) that the threading pass
makes as it reaches the end-point of the thread cutting pass. The end-point is
the X position programmed with the X-word. I is an incremental, signed distance
(+ or -) added to the X parameter to determine the start-point of the threading
pass on the X axis. If a chamfer is being cut at the end of the thread cutting
pass, it does not affect the value programmed here. This parameter should be
entered as if no chamfer were being cut. I is always an incremental value
regardless of the current mode. This parameter is always entered as a radius
value regardless of the current mode.
25-21