1
Chapter Two Programming
Chapter Two Programming
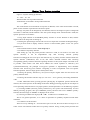
2.1 Block format
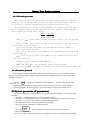
The block format means the written rules of block, it includes the function
which will be implemented by numerically controlled machine tool and parameters
that are required implementing this function. One part processing program is
composed of several blocks, and each block is composed of various functions;
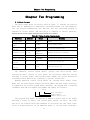
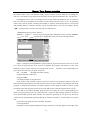
General function words of lathe numerical control system are as follows:
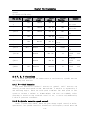
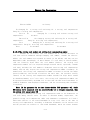
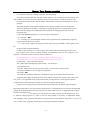
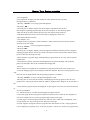
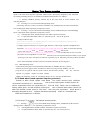
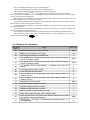
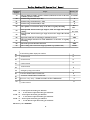
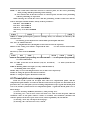
Table 2-1: Table of system function words
Function
Program number
Sequence segment
number
Preparatory
function
Address
Scope
Meaning
p、n
01~99
Specify
number
N
0~9999
Program segment number
G
00~99
Instruction movement mode
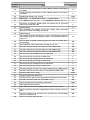
±0.001~
program number
and sub-program
Coordinate letter
X、I,K、
Feed speed
F
1~6000mm/min
Feed speed instruction
Spindle function
S
0~5000RPM
Instruction of spindle rotating speed
T
1~6
Cutting tool instruction
M
0~99
Auxiliary instruction
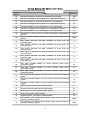
Cutting
function
Auxiliary
function
tool
Movement instruction coordinate,
±99999.999
The numerical control system doesn't require each block having these
instructions above, however in every block; the instruction should be arrived
according to certain format. Each function word probably has various definitions
in different block definitions, referring to specific instructions.
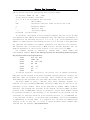
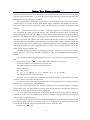
Washing numerical control system adopts the variable block format, which
means that the block length changes with word number and word length. One block
is composed of one or more program words. Generally, the program word is composed
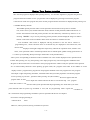
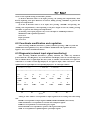
of address word and post-address word number and symbol, for instance:
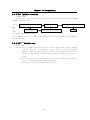
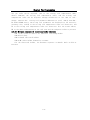
X
-
46.38
Data word (digit)
Symbol (minus)
Address function word
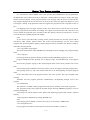
This program word format is composed of
following a string of digits, and several
written in the previous block and unchanged
can be no longer rewritten. In the dimension
2-1
address function word as the header
words compose one block. The words
in this block are also valid, which
words, it can only write valid digit