1
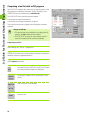
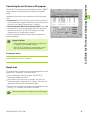
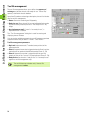
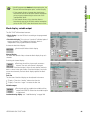
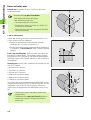
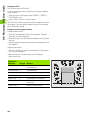
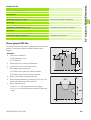
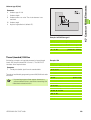
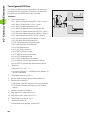
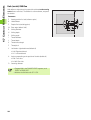
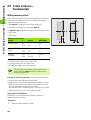
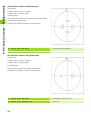
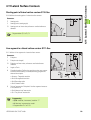
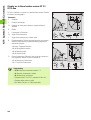
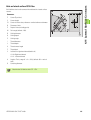
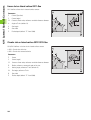
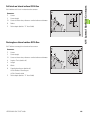
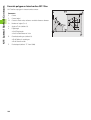
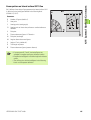
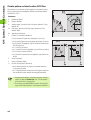
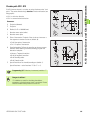
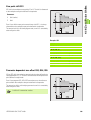
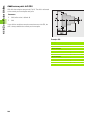
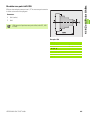
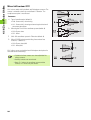
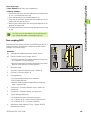
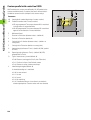
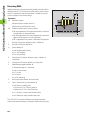
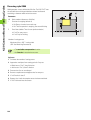
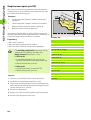
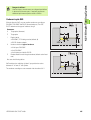
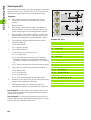
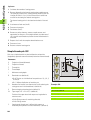
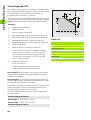
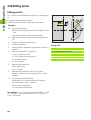
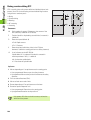
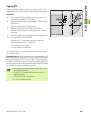
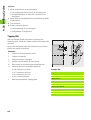
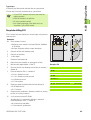
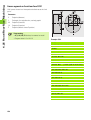
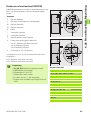
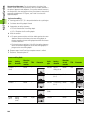
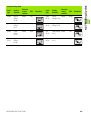
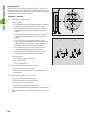
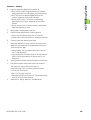
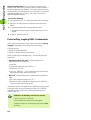
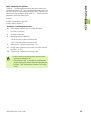
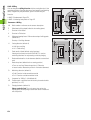
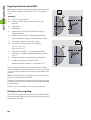
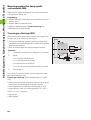
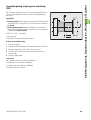
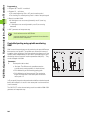
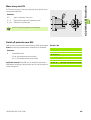
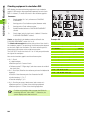
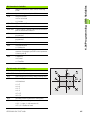
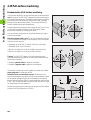
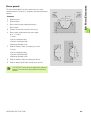
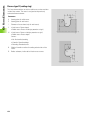
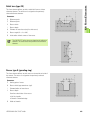
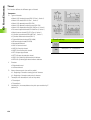
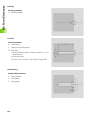
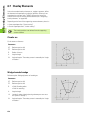
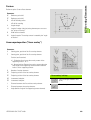
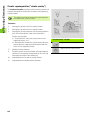
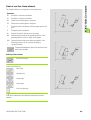
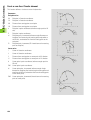
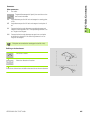
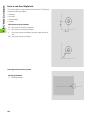
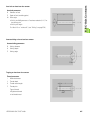
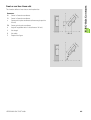
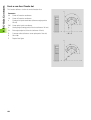
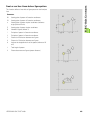
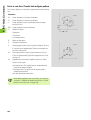
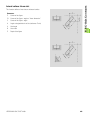
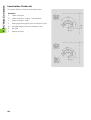
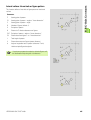
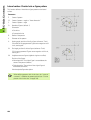
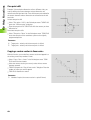
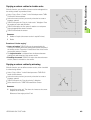
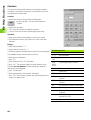
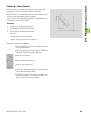
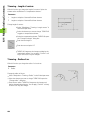
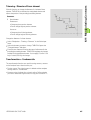
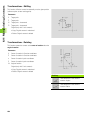
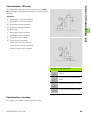
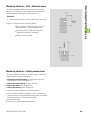
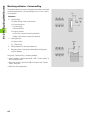
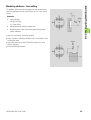
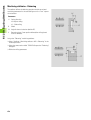
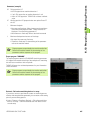
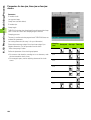
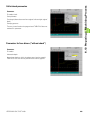
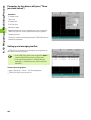
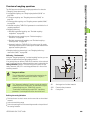
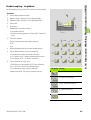
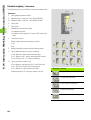
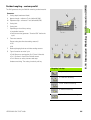
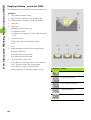
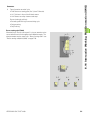
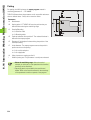
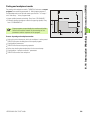
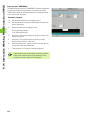
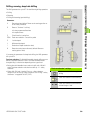
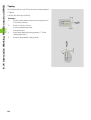
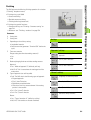
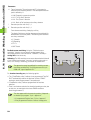
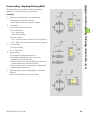
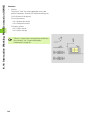
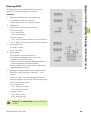
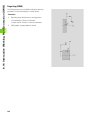
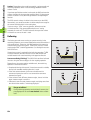
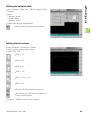
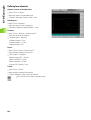
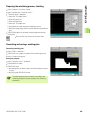
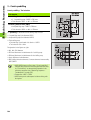
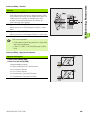
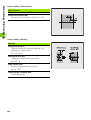
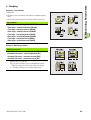
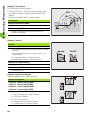
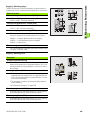
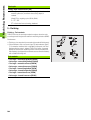
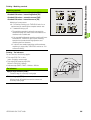
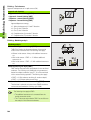
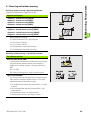
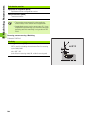
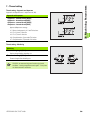
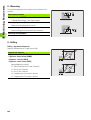
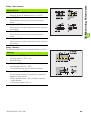
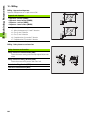
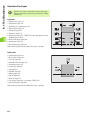
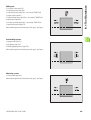
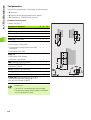
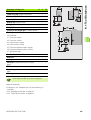
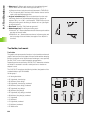
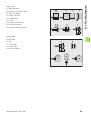
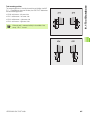
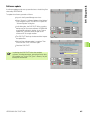
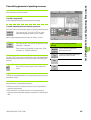
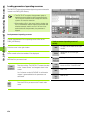
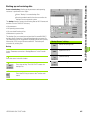
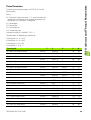
4.27 Milling Cycles 4.27 Milling Cycles Contour milling G840—Fundamentals G840 mills or deburrs open or closed contours (figures or “free contours”). Depending on the cutter, select vertical plunging or predrilling and then milling. Plunge strategies: Depending on the cutter you are using, select one of the following strategies: Vertical plunge: The cycle moves the tool to the starting point; the tool plunges and mills the contour. Calculate positions, predrill, mill. The machining process is performed in the following steps: Insert drill. Calculate hole positions with “G840 A1 ..”. Predrill with “G71 NF ..” Call cycle “G840 A0 ..”. The cycle positions the tool above the hole; the tool plunges and mills the contour. Predrilling, milling. The machining process is performed in the following steps: Drill holes with “G71 ..” Position the cutter above the hole. Call cycle “G840 A0 ..”. The cycle plunges and mills the contour or contour section. If the pocket consists of multiple milling contours, G840 takes all the sections of the contour into account for drilling and milling. Call “G840 A0 ..” separately for each section when calculating the hole positions without “G840 A1 ..”. Oversize: A G58 oversize “shifts” the contour to be milled in the direction given in “cycle type.” With inside milling and closed contour: Shifted inward With outside milling and closed contour: Shifted outward Open contour: Shifts to the left or right depending on Q If Q=0, oversizes are not taken into account. G57 and negative G58 oversizes are not taken into account. HEIDENHAIN CNC PILOT 4290 261