1
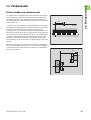
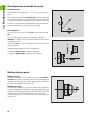
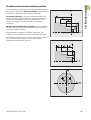
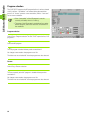
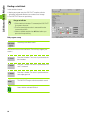
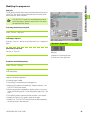
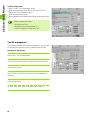
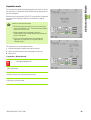
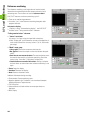
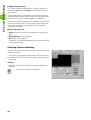
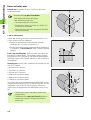
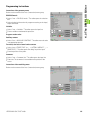
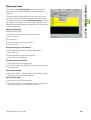
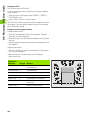
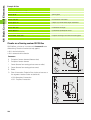
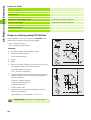
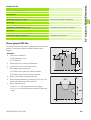
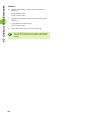
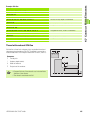
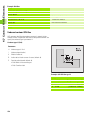
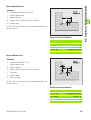
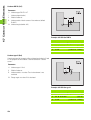
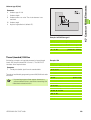
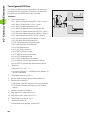
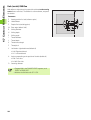
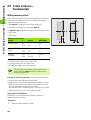
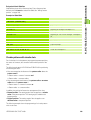
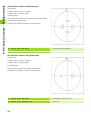
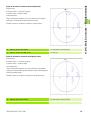
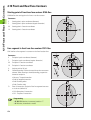
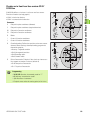
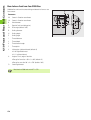
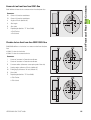
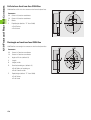
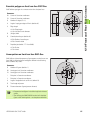
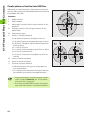
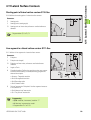
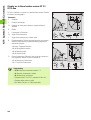
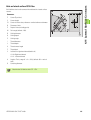
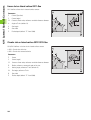
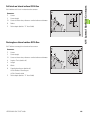
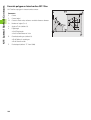
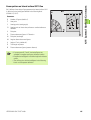
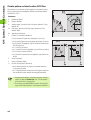
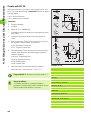
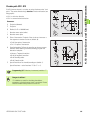
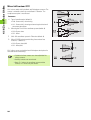
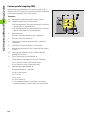
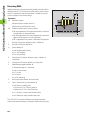
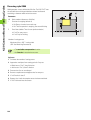
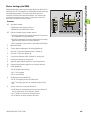
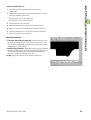
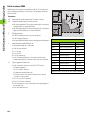
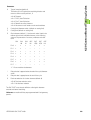
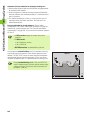
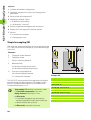
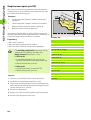
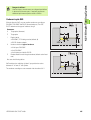
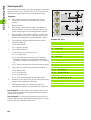
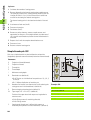
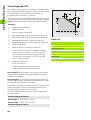
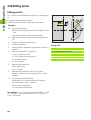
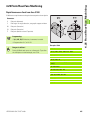
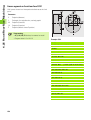
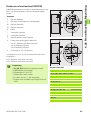
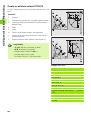
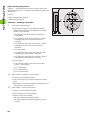
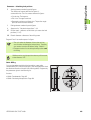
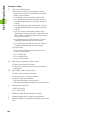
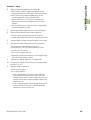
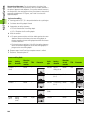
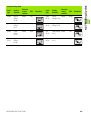
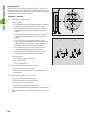
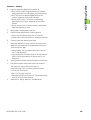
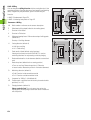
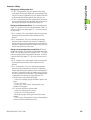
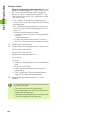
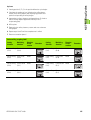
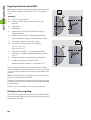
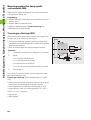
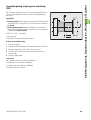
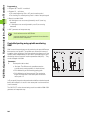
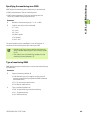
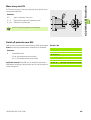
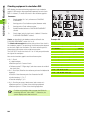
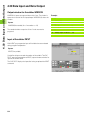
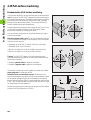
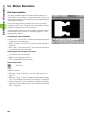
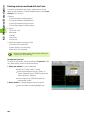
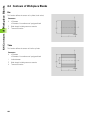
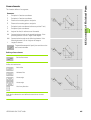
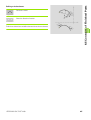
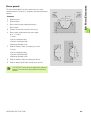
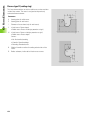
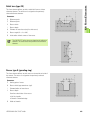
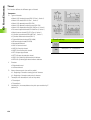
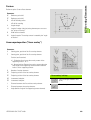
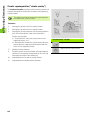
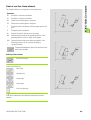
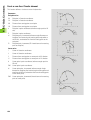
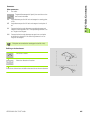
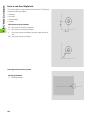
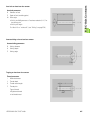
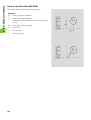
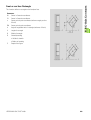
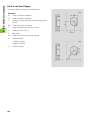
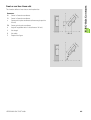
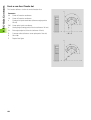
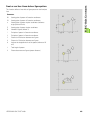
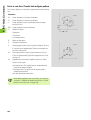
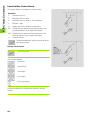
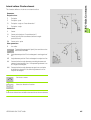
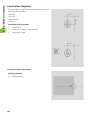
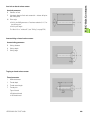
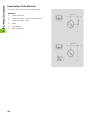
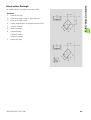
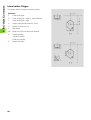
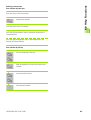
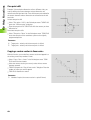
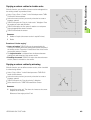
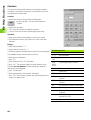
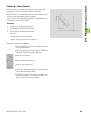
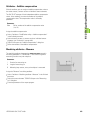
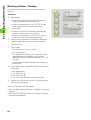
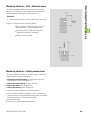
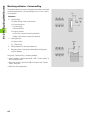
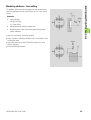
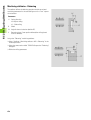
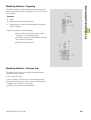
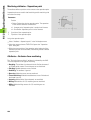
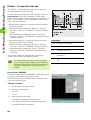
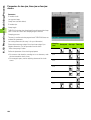
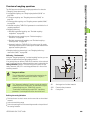
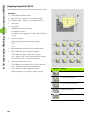
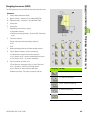
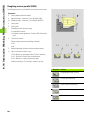
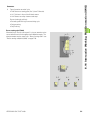
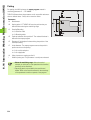
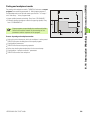
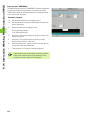
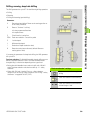
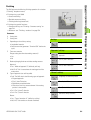
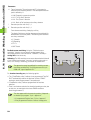
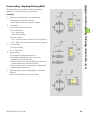
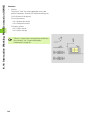
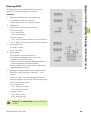
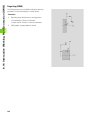
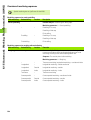
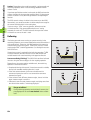
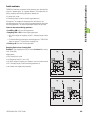
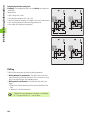
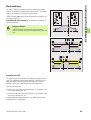
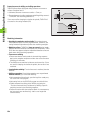
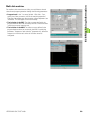
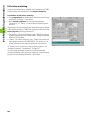
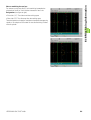
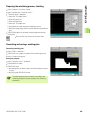
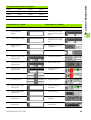
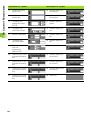
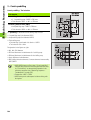
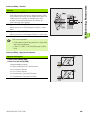
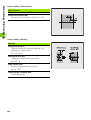
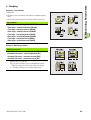
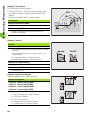
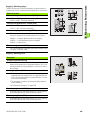
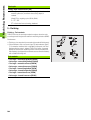
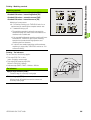
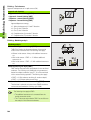
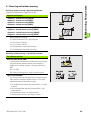
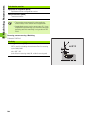
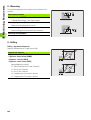
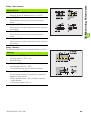
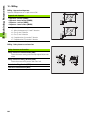
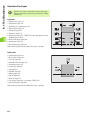
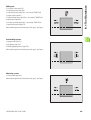
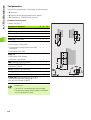
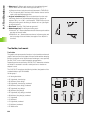
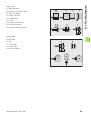
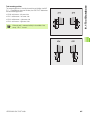
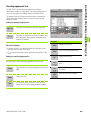
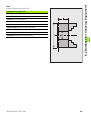
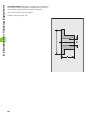
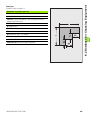
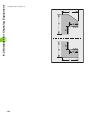
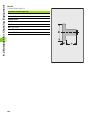
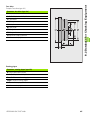
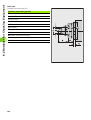
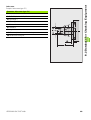
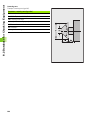
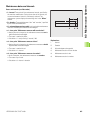
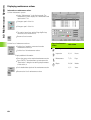
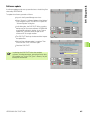
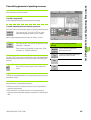
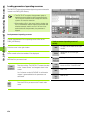
7.6 Machining Parameters Finishing – Tool tolerances Approach and departure are in rapid traverse (G0). Approach and departure Approach – external finishing [ANFA] Approach – internal finishing [ANFI] Departure – external finishing [ABFA] Departure – internal finishing [ABFI] Approach/departure strategy: 1: Move simultaneously in X and Z directions 2: First X, then Z direction 3: First Z, then X direction 6: Coupled motion; X precedes Z direction 7: Coupled motion; Z precedes X direction Finishing – Machining analysis Machining analysis Minimum finishing transverse length [FMPL] TURN PLUS checks the frontmost element of the outside contour to be finish-machined. The following rules apply: Without inside contour: Always with additional transverse cut With inside contour – FMPL >= l1: Without additional transverse cut With inside contour – FMPL < l1: With additional transverse cut Maximum finishing cut depth [FMST] FMST defines the permissible infeed depth for non-machined undercuts. The finishing cycle (G890) uses this parameter to determine whether undercuts (type E, F, G) will be machined with a contour-finishing operation. The following rules apply: FMST > ft: With undercut machining (ft: undercut depth) FMST <= ft: Without undercut machining Number of revolutions for chamfer or rounding [FMUR] The feed rate is reduced such that at least FMUR revolutions can be executed (evaluation: finishing cycle G890). The following rules apply to FMPL: The additional transverse cut is executed from the outside toward the inside. The “Transverse angle variation PWA” has no effect on the analysis of the transverse elements. 596